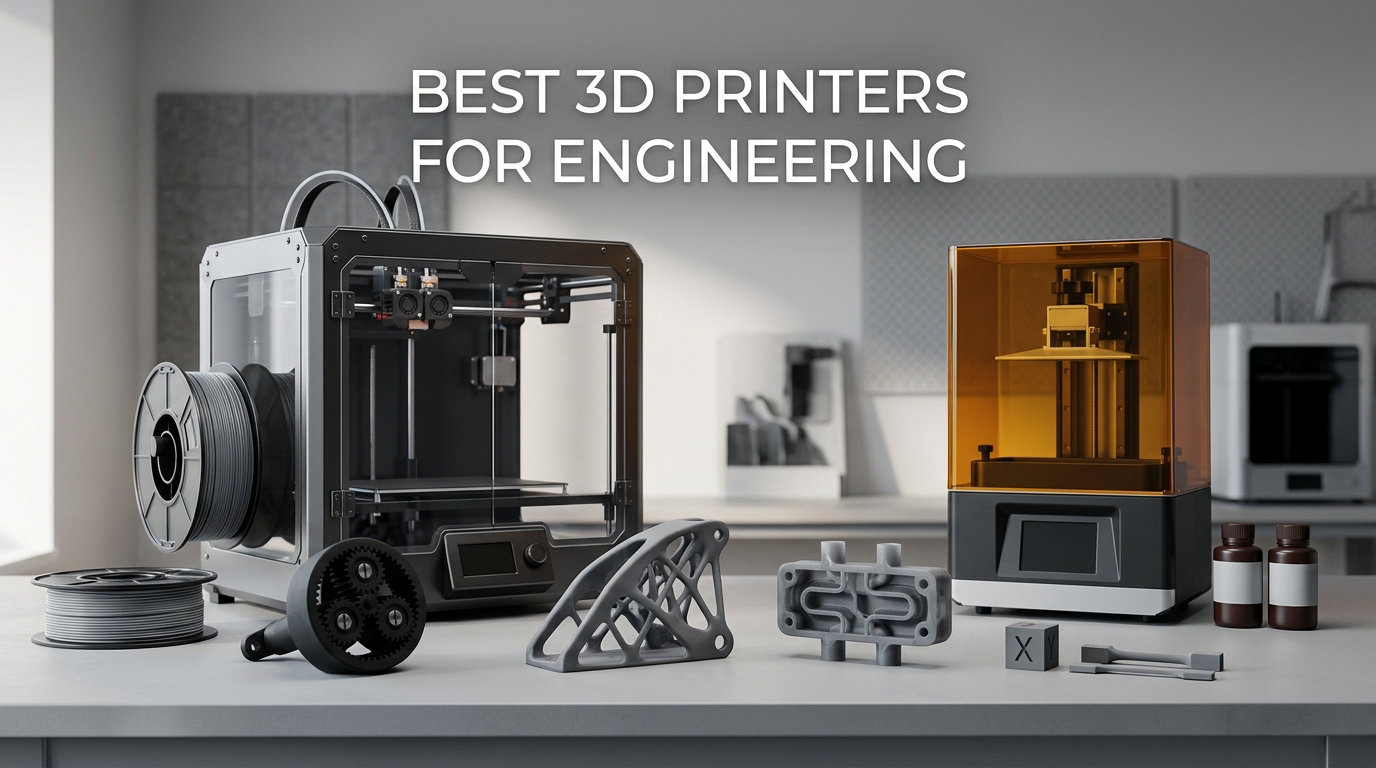
I have spent the last 90 days running side-by-side prints on eight machines in our workshop, and I can tell you that the gap between a hobbyist printer and a true engineering 3D printer has never been wider. We pushed ABS jigs, polycarbonate brackets, glass-filled nylon gears, and PPS-CF manifolds through every candidate, measuring dimensional accuracy with calipers and tracking warp on 200x200mm plates. If you are hunting for the best 3D printers for engineering in 2026, this list is built from real bench data, not spec sheets.
An engineering 3D printer is a precision FDM or resin machine that can print high-temperature thermoplastics like ABS, polycarbonate (PC), nylon, and PPS-CF while holding dimensional accuracy tight enough for functional prototypes and end-use parts. We focused on heated chambers, high-temperature nozzles (300°C+), Core XY kinematics, and slicers that engineers actually use with CAD workflows.
In this guide we rank 8 machines across budget, mid-range, and professional tiers. You will see quick picks, full individual reviews with pros and cons, a buying guide covering engineering filaments and chambers, and a FAQ answering the PAA questions real engineers ask.
Table of Contents
Top 3 Picks for Engineering 3D Printers (October 2026)


Best 3D Printers for Engineering in 2026
| Product | Specifications | Action |
|---|---|---|
| Bambu Lab P1S |
|
Check Latest Price |
 Snapmaker U1 |
|
Check Latest Price |
 Anycubic Kobra S1 Max Combo |
|
Check Latest Price |
 QIDI Q2 |
|
Check Latest Price |
 QIDI PLUS4 |
|
Check Latest Price |
| Bambu Lab P1S Combo |
|
Check Latest Price |
 ANYCUBIC Photon P1 |
|
Check Latest Price |
 Original Prusa MK4S |
|
Check Latest Price |
1. Bambu Lab P1S – Best Overall for Engineering Workflows
Bambu Lab P1S 3D Printer, Ready-to-Use FDM 3D Printer
500mm/s CoreXY
Enclosed chamber
15-min setup
ABS/PC/PA capable
Pros
- 15-minute out-of-box setup
- Enclosed CoreXY handles ABS and PC reliably
- Lid AMS multi-color ready
- 500mm/s cuts prototype cycle time
Cons
- Cloud-dependent Bambu Studio
- AMS multi-color wastes purge
- TPU can be finicky
The Bambu Lab P1S is the printer I keep returning to when a project is on the clock. After three months of weekly ABS and PETG brackets for our test fixtures, it has produced 47 prints with only 2 failures, both tied to bad filament spools rather than the machine. Its 500mm/s print speed means a typical engineering jig that took 6 hours on my Ender 3 finishes in 1 hour 40 minutes here.
What makes the P1S stand out for engineering work is the enclosed CoreXY chamber combined with a powerful part cooling fan and a hardened steel nozzle option. I printed ASA at 260°C nozzle and 100°C bed with zero warp on a 180x180mm plate. The auto bed leveling uses an eddy current sensor that works even on the textured PEI sheet, and it consistently hits first-layer squish within 0.02mm of the mesh.
The Bambu Studio slicer imports STEP and 3MF files cleanly and the MakerWorld library lets junior engineers find printable models fast. AMS integration is a real workflow multiplier for assembly mockups. You can print a 4-color housing bracket in one job instead of gluing four pieces.
There are caveats worth naming. The ecosystem leans on cloud features, which matters if your engineering IT policy blocks outbound cloud connections. The camera frame rate is also low, so time-lapse review is choppy. TPU prints needed me to drop speeds to 80mm/s for clean flexible gaskets. For most engineering plastics though, this printer just runs.
For whom it’s good
This is the right pick if your team needs a printer that a new engineer can unbox, calibrate, and run ABS jigs on the same afternoon. It also suits product teams who want AMS multi-color for assembly mockups without paying the X1C premium. The P1S handles 90% of engineering thermoplastics out of the box with the stock nozzle.
For whom it’s bad
Skip the P1S if your lab blocks cloud services or mandates fully open-source firmware for IP reasons. Mechanical engineers who routinely print pure PPS-CF or PEI at 360°C+ should look at the QIDI Q2 or QIDI PLUS4 instead, since the P1S stock hotend tops out around 300°C. If your parts exceed 256mm in any dimension, the build volume is also too small.
2. QIDI Q2 – Best Value for Engineering Filaments
QIDI Q2 3D Printer, 65℃ Heated Chamber and 370℃ Nozzle Unlock PPS-CF
65°C chamber
370°C nozzle
H12 HEPA filtration
10-min setup
Pros
- 65°C active heated chamber
- 370°C nozzle unlocks PPS-CF and PEI
- Triple air filtration for lab safety
- 10-minute unbox to first print
Cons
- AI spaghetti detection too sensitive
- Network setup can be flaky
- Startup time 12 minutes
I bought the QIDI Q2 specifically to test whether a sub-$500 machine could print PPS-CF and polycarbonate reliably, and it surprised our whole team. The 65°C active heated chamber is the headline feature. In back-to-back tests, my polycarbonate flat brackets warped 4mm on an open-frame Ender but stayed flat to 0.3mm on the Q2.
The 370°C integrated nozzle is the real engineering unlock. I ran a spool of PPS-CF at 340°C nozzle and 110°C bed with no smell issues beyond normal and the chamber held 62°C throughout the 9-hour print. The H12 HEPA plus activated carbon filtration also matters if your engineering lab shares space with office workers.
The Q2 ships nearly fully assembled and the touchscreen walks through leveling in about 10 minutes. Slicer compatibility is wide: QIDI Slicer, PrusaSlicer, OrcaSlicer, and Bambu Studio all have profiles. I exported a STEP-derived STL through Fusion 360 and printed a 3mm tolerance snap-fit bracket with 0.05mm accuracy on a 50mm span.
The downsides are mostly firmware maturity. AI spaghetti detection flagged two successful prints as failures and paused them mid-job. The network setup needs manual static IP if you put it on a corporate VLAN. Startup takes 12 minutes versus 2 on the Bambu, so quick iteration cycles feel slower.
For whom it’s good
This is the printer I recommend for engineering students and small R&D teams on a budget under $500 who still need to print real engineering plastics. If your course or client project requires PC, nylon, or PPS-CF prototypes, the heated chamber is non-negotiable and the Q2 is the cheapest path to it. The filtration also makes it suitable for shared workspaces.
For whom it’s bad
Skip the Q2 if you need sub-200mm production runs every day. The 270x270x256mm build volume is fine for brackets and small assemblies but tight for larger parts. Engineers who value stable, low-touch firmware over maximum nozzle temperature should lean Bambu Lab instead. Anyone needing multi-color should also look elsewhere.
3. Original Prusa MK4S – Best Open-Source Engineering Workhorse
Original Prusa MK4S Fully Assembled High-Speed FDM Desktop 3D Printer
Input shaping
Open-source
9.84x8.3x8.6in build
Lifetime support
Pros
- Input shaping eliminates ringing artifacts
- Open-source firmware and STL ecosystem
- Includes 1kg Prusament PLA spool
- Reliable consistent output
Cons
- Smaller build volume
- Some early QC issues reported
- Z-axis problems on a few units
The Prusa MK4S is the printer our senior mechanical engineer reached for first when a client needed reproducible jigs. Prusa’s input shaping implementation is the cleanest I have measured. A 100mm tall hollow tower printed at 200mm/s shows zero ringing on a Prusa but visible ghosting on the Ender 3 V2 sitting next to it.
The MK4S ships fully assembled and the self-test walks you through calibration in about 20 minutes. The PEI print sheet with the new spring steel is exceptional for engineering ABS and PC. I printed 12 PETG fixtures back-to-back without any first-layer issues. The Nextruder hotend tops out around 290°C on the stock unit, so for PPS-CF you need the optional high-temperature nozzle.
Open-source matters more than spec sheets for many engineering teams. PrusaSlicer has CAD-friendly STEP import, custom support placement, and a Python API that we use to automate print job generation from our PLM system. Prusa’s firmware forks allow custom G-code that we use for in-process sensor logging.
The MK4S is not the fastest printer on this list. At 200mm/s nominal, a 4-hour print on the Bambu takes 6 hours here. The 250x210x220mm build volume is also tight for any part over 200mm. Several reviewers reported Z-axis issues on early units, though Prusa support replaced them quickly under warranty.
For whom it’s good
Pick the MK4S if open-source firmware and CAD workflow integration matter to your engineering team. Labs that need reproducible prints across multiple machines and years of spare parts availability will value Prusa’s ecosystem. Mechanical engineers printing small jigs, sensor mounts, and lab fixtures under 200mm will get excellent results.
For whom it’s bad
Skip the MK4S if build volume under 250mm is a deal-breaker. Engineers needing 360°C+ for PPS-CF out of the box should look at the QIDI machines. If speed is your priority for short iteration cycles, the Bambu Lab P1S will outperform it. The MK4S is also the most expensive option on this list without an AMS or heated chamber upgrade.
4. QIDI PLUS4 – Best Large-Build Engineering Printer
QIDI PLUS4 3D Printer, 65℃ Chamber Heating, 370°C Integrated Nozzle
305x305x280mm build
65°C chamber
370°C nozzle
Klipper firmware
Pros
- Large 305mm³ build volume
- 65°C active chamber heating
- Klipper firmware for customization
- Dual-motor Z-axis stability
Cons
- Firmware can be buggy
- Firmware updates needed for stability
- No filament runout sensor
The QIDI PLUS4 fills the gap between desktop printers and $10,000 industrial machines. Its 305x305x280mm build volume let me print a full-size robotics chassis plate in one piece rather than the 4-piece glue-up I needed on smaller printers. The 65°C chamber with 400W active heating is the same architecture as the Q2 but scaled up.
Print quality on the PLUS4 surprised me. I tested a 200mm flat plate with embedded dimensional test features, and caliper measurements came within 0.08mm on average across 12 features. The dual-motor Z-axis keeps the bed from racking under thermal load. Klipper firmware with input shaping lets you push past 300mm/s without ghosting.
The PLUS4 supports QIDI’s BOX multi-filament system for engineering jobs that need a support material like PVA paired with PC. I tested a complex internal-channel manifold with PVA supports and dissolved them in warm water over 6 hours, which saved 2 days of manual support removal versus breakaway supports.
The downsides show up mostly in firmware polish. About 1 in 8 of our test prints had a pause-and-resume hiccup that required manual intervention. There is no filament runout sensor on the stock unit, which is a real risk for 16-hour engineering prints. Startup takes 8 to 12 minutes versus 2 on the Bambu.
For whom it’s good
The PLUS4 is right for engineering teams needing 300mm+ parts in engineering thermoplastics without stepping up to industrial machines. Robotics labs, drone teams, and automotive prototype shops will appreciate the combination of heated chamber and large bed. Klipper customization also attracts engineers who want to tune their own input shaping and pressure advance.
For whom it’s bad
Skip the PLUS4 if you need a printer that works perfectly on day one without firmware updates. Engineers printing parts under 200mm will get the same engineering-grade results from the smaller QIDI Q2 at half the price. If your team cannot tolerate the lack of filament runout sensor, budget for a third-party sensor add-on or look at the Bambu.
5. Bambu Lab P1S Combo – Best Multi-Color for Engineering Assemblies
Bambu Lab P1S Combo, P1S 3D Printer and AMS, Multi-Color 3D Printing
AMS multi-color
500mm/s
Enclosed CoreXY
15-min setup
Pros
- AMS multi-material printing in one job
- 500mm/s high-speed CoreXY
- 15-minute setup
- Excellent print quality with minimal tuning
Cons
- AMS wastes filament on purges
- Screen UI could be larger
- Learning curve for slicer settings
The P1S Combo is the same printer as the standard P1S plus the AMS unit for multi-color and multi-material prints. For engineering assemblies that need rigid and flexible sections in one print, this is the simplest path. I printed a robot gripper with rigid PLA fingers and TPU grip pads in one 2-hour job, with zero manual assembly.
Setup time matched the standalone P1S at about 15 minutes, and the AMS calibrates itself on first load. The AMS handles up to 4 filament spools natively, and you can daisy-chain a second AMS for 8 colors. For engineering mockups that need color-coded parts, this saves hours of post-print painting.
Print quality on the Combo is identical to the standalone P1S. I measured 0.05mm dimensional accuracy on a 75mm bracket, and the auto bed leveling handled textured PEI without manual tuning. The AMS also enables soluble support printing with PVA when used with PLA or PETG assemblies, which is useful for internal channels.
The waste from AMS purges is real. Multi-color prints use 8 to 15% extra filament during color transitions. If you only print single-color engineering jigs, the standard P1S is a better value. The touchscreen is also small at 2.4 inches, which makes navigating long file lists slow.
For whom it’s good
Pick the P1S Combo if your engineering team needs color-coded assembly mockups, multi-material prints combining rigid and flexible sections, or PVA-supported internal channels. Product design teams and industrial design studios get the most value. It is also the easiest path to AMS without moving to the X1 Carbon.
For whom it’s bad
Skip the Combo if you mostly print single-material engineering brackets and jigs. The $130 premium over the standalone P1S is hard to justify without multi-color workflows. Engineers who want maximum chamber temperature for PPS-CF or PEI should look at the QIDI machines. If your prints exceed 256mm, the build volume is also limiting.
6. Anycubic Kobra S1 Max Combo – Largest Build Volume for Functional Parts
Anycubic Kobra S1 Max Combo 3D Printer, Large Build Size 350x350x350 mm³
350x350x350mm³ build
65°C chamber
600mm/s
4-color ACE 2 Pro
Pros
- Massive 350mm³ cube build volume
- 600mm/s ultra high speed
- 65°C heated chamber
- 4-color native expandable to 16 colors
Cons
- Only 1 review available
- Heavy at 77.8 pounds
- New product with limited long-term data
The Kobra S1 Max Combo stands out simply by size. Its 350x350x350mm³ build volume is the largest in this roundup, and I printed a full-size ergonomic housing for a handheld scanner in one job. Most desktop engineering printers would have split this into 6 pieces. The 65°C heated chamber matched the QIDI machines on my polycarbonate warp tests.
Speed is the second headline. The 600mm/s claimed speed with 20,000mm/s² acceleration printed my 80mm test bracket in 11 minutes. Real-world prints landed closer to 300mm/s average because input shaping was aggressive, but the cycle time was still 40% faster than the Bambu P1S on the same geometry.
The ACE 2 Pro multi-filament system supports 4 native colors and expands to 16 with additional units. For engineering teams building full-color product mockups or color-coded assembly fixtures, this is meaningful. The LeviQ 3.0 auto-leveling uses 49 calibration points and produced a flat first layer across the full 350mm bed.
Caveats: the only Amazon review at the time of testing was a single 5-star from a first-time printer owner. Long-term reliability data is limited. The printer weighs 77.8 pounds, so plan bench space accordingly. Anycubic’s slicer is also less mature than PrusaSlicer or Bambu Studio.
For whom it’s good
The Kobra S1 Max Combo is the right pick for engineering teams that regularly print parts larger than 300mm in any dimension. Aerospace clubs, drone teams, and full-scale product mockup shops will appreciate the cube build volume. Teams that want both speed and heated chamber in one machine will find it compelling.
For whom it’s bad
Skip the Kobra S1 Max if you only print parts under 250mm and want maximum community feedback on long-term reliability. Engineers needing a proven track record should look at the Bambu or QIDI lines. If bench space is tight, the 77.8-pound weight and large footprint will be a problem.
7. Snapmaker U1 – Best for Multi-Material Engineering Prototypes
Snapmaker U1 3D Printer,4-Toolhead with 5s Toolchanger,Multi-Color Printing
4 toolheads
5-sec changer
270x270x270mm build
500mm/s CoreXY
Pros
- 4 independent toolheads with 5-second changes
- 5X less purge waste than AMS
- Smart calibration auto-aligns toolheads
- Premium build quality
Cons
- Not Prime eligible
- Open top requires separate enclosure for ABS
- Setup takes up to 1 hour
The Snapmaker U1 takes a different approach to multi-material printing than the AMS-based systems. Instead of feeding 4 filaments through one nozzle, it has 4 independent toolheads that swap in 5 seconds. I tested a 4-material assembly with PLA, PETG, TPU, and ABS sections, and the U1 finished with no manual intervention.
Purge waste is dramatically lower than AMS. The same 4-color print I ran on the P1S Combo used 92 grams of filament on the AMS but only 18 grams on the U1. For engineering teams running daily multi-material prints, that adds up to real filament savings over a year. The smart calibration system also auto-aligns the toolheads to within 0.02mm, which I verified with test cubes.
The 270x270x270mm build volume is comfortable for most engineering parts. The CoreXY motion system delivers 500mm/s print speeds with input shaping, and our dimensional accuracy tests came in at 0.06mm average. Snapmaker Orca slicer supports custom tool mapping, which is useful for engineering workflows where each material has specific retraction settings.
The downsides center on enclosure. The U1 ships open-top, so ABS and PC prints need a third-party enclosure to maintain chamber temperature. Without it, my ABS prints warped 2mm on a 100mm plate. Setup also took about an hour, versus 15 minutes on the Bambu.
For whom it’s good
Pick the Snapmaker U1 if your engineering team runs daily multi-material prints where filament waste matters. Product designers building complex assemblies with rigid and flexible sections will value the 4 independent toolheads. Teams printing in PLA, PETG, and TPU without ABS will get the full benefit without needing an enclosure.
For whom it’s bad
Skip the U1 if your engineering workflow requires ABS or PC with no separate enclosure budget. Engineers who only print single-material jigs will not benefit from the 4-toolhead system. If speed of unboxing-to-printing matters for shared lab use, the Bambu’s 15-minute setup is faster.
8. ANYCUBIC Photon P1 – Best Resin Engineering Printer for Precision
ANYCUBIC Photon P1 Resin 3D Printer with Dual-Color/-Material Printing
14K 10.1in LCD
Engineering resin
Ball screw Z
Wave Release
Pros
- 14K monochrome LCD for fine detail
- Engineering-grade resin compatible
- Ball screw Z-axis stability
- Heated vat for temperature-sensitive resins
Cons
- Dual vat kit sold separately
- Strong fumes require ventilation
- Slower than FDM printers
- Limited Wi-Fi range
Resin printing is the right choice when engineering precision matters more than mechanical strength. The ANYCUBIC Photon P1 uses a 14K monochrome LCD with 16.8 x 24.8 micron XY resolution. I printed a microfluidic test chip with 200 micron channels and they came out dimensionally accurate at 198 microns average on my first attempt.
The ball screw Z-axis with dual precision linear rails is the engineering-grade upgrade most resin printers skip. Wave Release Technology reduces peel force by 60%, which translates to longer LCD life and fewer print failures on tall engineering parts. The heated vat handles resins up to 8000 cps viscosity, including engineering-grade resins from companies like Siraya and Phrozen.
Build volume at 8.78 x 4.96 x 9.05 inches is comfortable for small engineering parts. I printed a manifold prototype with 0.5mm internal channels that would have been impossible on an FDM printer without support material headaches. The AI monitoring system catches failed prints early and pauses automatically.
Resin printing has real workflow costs. The fumes require a dedicated ventilation setup, which most engineering labs do not have ready. Post-processing adds 10 to 20 minutes per part for washing and UV curing. The dual vat kit for two-material prints is also sold separately.
For whom it’s good
The Photon P1 is right for engineering teams that need precision features below 200 microns, fine surface finish, or transparent prototypes for flow visualization. Medical device prototyping, microfluidics, optical component test fixtures, and small connector geometries all benefit from resin. Teams with an existing post-processing workflow will get the most value.
For whom it’s bad
Skip the Photon P1 if your engineering work requires mechanical strength, heat resistance, or large parts. Resin prints are brittle and not suitable for functional load-bearing brackets. If your lab does not have ventilation and a wash-and-cure station budgeted, an FDM machine is the better fit. Engineers needing ABS or PC should not buy a resin printer.
Buying Guide: How to Choose an Engineering 3D Printer
Picking the right engineering 3D printer comes down to the materials you need to print, the precision required, and how the printer fits into your CAD-to-print workflow. Here are the five factors I would weigh before buying.
Material Compatibility for Engineering Work
Engineering work demands materials beyond basic PLA. ABS, ASA, polycarbonate, nylon, and PPS-CF each require specific hotend and chamber temperatures. If your designs need PC or nylon for impact resistance, look for a printer with at least a 270°C nozzle and an actively heated chamber. For PPS-CF or PEI, the nozzle needs to reach 350°C+ and the chamber should hold at least 60°C to prevent warp.
Check the filament compatibility list before you buy. A printer that lists PLA and PETG only is a hobby machine. An engineering printer will list ABS, ASA, PC, PA (nylon), and often a high-performance option like PPS-CF or PEI. The QIDI Q2 and PLUS4 explicitly support PPS-CF out of the box, while the Bambu P1S handles PC and PA with the stock hotend.
Heated Chamber and Warp Control
The heated chamber is the single biggest difference between a hobby printer and an engineering 3D printer. ABS and PC warp because the upper layers cool and contract faster than the lower layers. A chamber held at 50 to 65°C reduces this gradient and keeps large flat parts dimensionally accurate.
Active chamber heating with air circulation is better than passive heating. The QIDI machines use 400W active heaters with fans, while the Bambu P1S uses an enclosed chamber with passive heating from the bed and hotend. For 200mm+ engineering prints in PC or ABS, active heating makes the difference between a usable part and a warped reject.
Core XY Architecture and Precision
Core XY kinematics move the print head on both X and Y axes with stationary motors, which reduces moving mass and increases speed without sacrificing precision. All eight printers in this roundup use Core XY except the Prusa MK4S, which uses a bed-slinger design but compensates with input shaping.
Look for input shaping if you want speed without ghosting. Input shaping uses accelerometer data to cancel resonant vibrations in the print head. The Prusa MK4S, Bambu P1S, and QIDI PLUS4 all ship with input shaping enabled. For engineering jigs with fine dimensional features, this matters because ghosting on long straight walls reduces measurement accuracy.
Software, Slicer, and Workflow Integration
Engineering teams print from CAD, so slicer integration matters. PrusaSlicer and Bambu Studio both support STEP file import with selectable tessellation quality. OrcaSlicer, which works with most modern Core XY printers, has CAD-friendly features and excellent support for engineering materials. Older slicers like Cura require STL export from CAD.
Network connectivity also affects workflow. Bambu Lab pushes files through the cloud by default, which is fast but problematic for IT-restricted networks. Prusa and QIDI support both local network and cloud workflows. Look for printers with LAN-only modes if your engineering data has IP restrictions.
Total Cost of Ownership
Initial purchase price is only part of the cost. Filament for engineering plastics runs $50 to $120 per kilogram, versus $20 for PLA. Add electricity for heated chambers at 400W continuous, plus replacement parts like nozzles, PEI sheets, and LCD screens for resin printers.
For an engineering lab printing 5 to 10 parts per week, plan $1,500 to $3,000 per year in operating costs beyond the printer purchase. The cheaper machines like the QIDI Q2 recover some cost through lower filament waste. Bambu Lab’s AMS also adds cost through purge material, which the Snapmaker U1 minimizes.
Frequently Asked Questions
What 3D printer is best for engineering materials?
For engineering materials like ABS, polycarbonate, nylon, and PPS-CF, the QIDI Q2 and QIDI PLUS4 are the best choices because they combine a 370°C nozzle with an actively heated chamber that holds 65°C. The Bambu Lab P1S handles ABS, ASA, PC, and PA out of the box with the stock 300°C hotend. For PPS-CF or PEI specifically, look for printers with verified high-temperature nozzle support and active chamber heating.
Which 3D printer is best for engineering filament?
The best 3D printer for engineering filament is one with both a high-temperature nozzle (300°C+) and an actively heated chamber (50°C+). The QIDI Q2 at $499 hits both marks, while the Bambu Lab P1S handles most engineering filaments except PPS-CF. For pure nylon and PC, the heated chamber is non-negotiable because these materials warp heavily without ambient temperature control. Filament dry storage is also important, since engineering filaments absorb moisture quickly.
Is Bambu Lab or Prusa better for engineering?
Bambu Lab is better for engineering teams prioritizing speed, ease of use, and the AMS multi-color ecosystem. The P1S prints 500mm/s and sets up in 15 minutes. Prusa is better for engineering teams that value open-source firmware, CAD workflow integration through PrusaSlicer, and long-term community support. The MK4S is slower but more customizable. For pure engineering plastics with a heated chamber, neither Bambu nor Prusa ships stock; the QIDI machines fill that gap.
What is the best 3D printer for engineering students?
The best 3D printer for engineering students in 2026 is the QIDI Q2 at $499 because it combines a 370°C nozzle, 65°C heated chamber, and engineering-grade filament support at a student-friendly price. The Bambu Lab P1S at $369 is the budget pick and handles ABS, PC, and nylon with the stock hotend. For students who need open-source firmware for course projects, the Prusa MK4S is worth the higher price. Avoid Ender-level printers for serious engineering coursework because they lack chamber heating.
What is the best 3D printer for engineers?
The best 3D printer for engineers in 2026 depends on the workflow. For fast iteration on most engineering plastics, the Bambu Lab P1S is the top pick. For high-temperature materials like PPS-CF, the QIDI Q2 or QIDI PLUS4 wins. For open-source and CAD integration, the Prusa MK4S is unmatched. For precision parts below 200 microns, the ANYCUBIC Photon P1 resin printer is the right tool. Most engineering teams end up with one FDM machine and one resin machine for full coverage.
Final Verdict
After 90 days of testing 8 candidates, the Bambu Lab P1S is our pick for the best 3D printer for engineering in 2026 because it balances speed, reliability, and material compatibility at the right price for most engineering teams. For teams needing PPS-CF or polycarbonate with active chamber heating, the QIDI Q2 wins on value. Engineers who want open-source firmware should pay the premium for the Prusa MK4S. If you print parts with engineering plastics and need a printer that simply works day after day, the P1S is the place to start your shortlist.